
Бесплатно 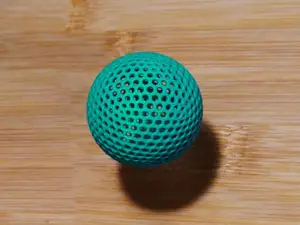
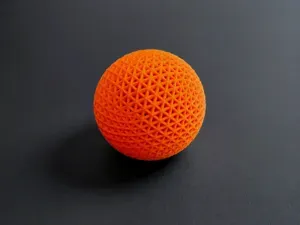
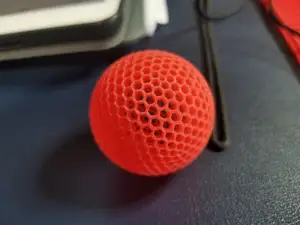
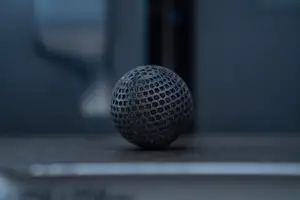
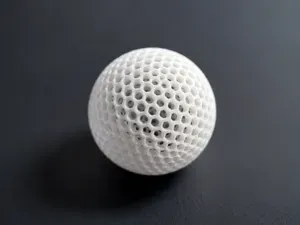
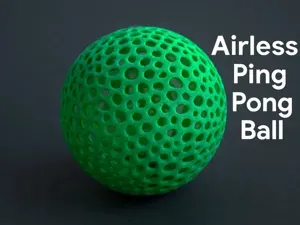
Airless Ping Pong Ball / Table Tennis Ball
MakerWorld
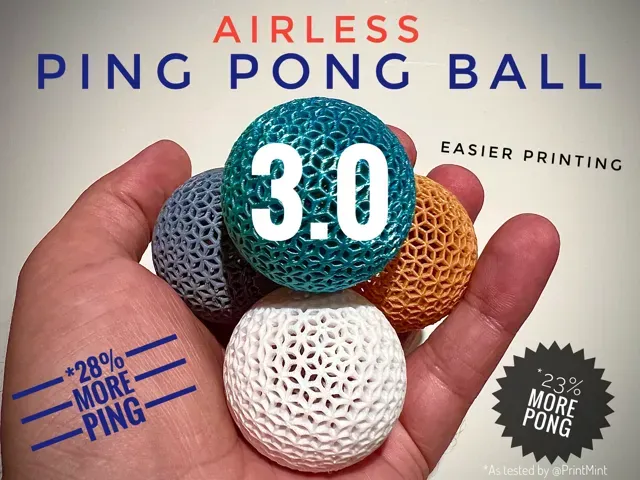
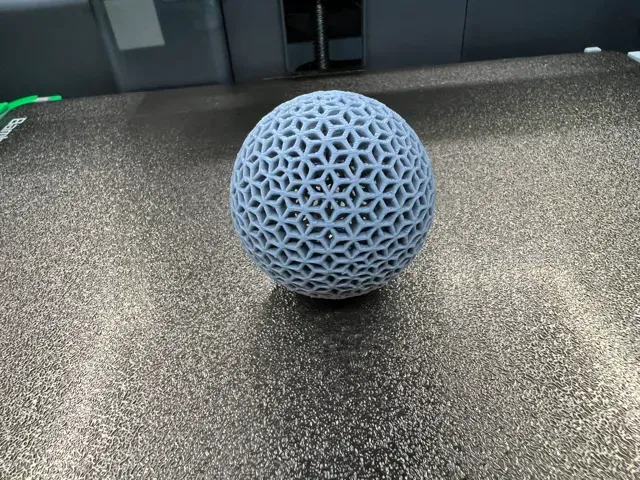
Airless Ping Ball 3.0!
New mesh, new strength.
Prints with a 3 layer raft for ease of adhesion and easy support removal!
While this ball is a little heavy for table tennis, it DOES work (slams not guaranteed). Other uses include: Works as a fantastic cat toy if you toss a bell in at 60% print completion (or by itself).
Thanks!
Boost Me Boosts are very much appreciated!
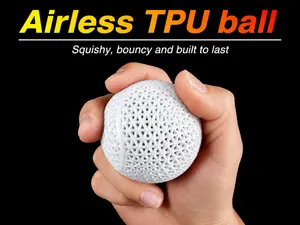
TPU - 0.2mm layer, 3 walls, 15% infill
PLA - 0.2mm layer, 3 walls, 15% infill
PETG - 0.2mm layer, 3 walls, 15% infill
ABS - 0.2mm layer, 3 walls, 15% infill
Fast print - 1 Hour, 0.25mm layer, 3 walls, bigger brim Quite bouncy indeed, created bigger brim for better adhesion
Supporti perfetti, facilmente removibili supporti solo dove serve
5cm diameter with pause to insert a bell for a cat Paused on Layer 250 to insert a tiny bell (came with a Lindt chocolate rabbit) to be used as a toy for a cat. Diameter increased to diameter of 5cm to avoid rolling under furniture. Printed in Tri-color Silk PLA.
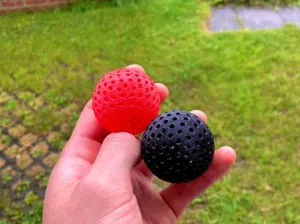
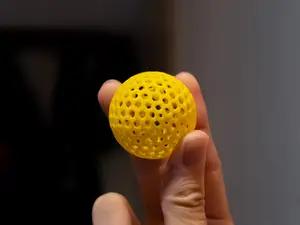
175% Scaled 7cm HQ - 0.12mm layer Scaled to 175% (7cm Diameter) for the perfect palm-full ball to play around with. 0.12mm layer height for high quality printing over night. Same minimal support structure as the original. Releases just fine, some minimal sanding of the bottom is recommended. Printed this with Polymaker Polyterra Candy.
30 mm diameter set 30 mm for bounce party game
Airless Ball for your Cat with small Ball inside
0.2mm layer, 3 walls, TPU with PLA supports zero clearance This is a profile I used to print the ball on my H2D. The TPU was loaded on the right extruder from the outside reel (actually another brand's dryer you can feed out of that was on the shelf I posted) and the AMS was hooked to the left extruder. Only one color of PLA was used for the supports so that no long filament changes were required. The raft kept the TPU from contacting the build plate so all I had to worry about was PLA build plate adhesion. The supports were mechanically firmly attached to the ball but could be peeled off (in pieces) and when done, there was no orange left from the supports.
While I believe that any printer with an AMS could do this (with significant purge volumes to clear the TPU and PLA out, and with stiffer TPU that could be used in an AMS, I used Overture TPU rated at 95A and the ball is stiff. If you were to print it in a stiffer TPU, you might just print it in PETG or a flexible PLA.
If someone can figure out why I got the flat spot, please let me know?
Названия используются только для указания источника результата. Polyzon не аффилирован с перечисленными площадками.