
Бесплатно 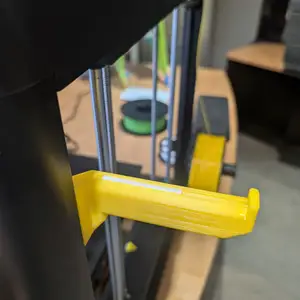
Ender 5 Max Front Filament Arm
Creality Cloud


Start G-Code:
M211 S0 ; disable travel limits G92 E0 ;reset extruder G28 ;home M420 S1 Z10 ;use bed mesh G1 Z10.0 F4000 move Z axis G1 X-10 Y20 Z10 F5000.0 ;move to start position G92 E0 ;zero the extruded length G1 F200 E10 ;extrude ooze G92 E0 ;zero the extruded length G1 Z1.0 F4000 ;move Z axis End G-Code:
G91 ;Relative positionning G1 E-2 F1500 ;Retract a bit G1 E-2 Z0.2 F1500 ;Retract and raise Z G1 X5 Y5 F3000 ;Wipe out G1 Z10 ;Raise Z more G90 ;Absolute positionning
G1 X0 Y0 ;Present print M106 S0 ;Turn-off fan M104 S0 ;Turn-off hotend M140 S0 ;Turn-off bed
M84 X Y E ;Disable all steppers but Z




Названия используются только для указания источника результата. Polyzon не аффилирован с перечисленными площадками.
Комментарии